Engineering review
We align the base and clad grades, thicknesses, dimensions, code requirements and intended fabrication.
Technology / Controlled energy
Explosion bonding joins dissimilar metals in a solid state. Our work is the engineering around that instant: surface preparation, geometry, energy control, recovery and proof.
01 / Manufacturing route
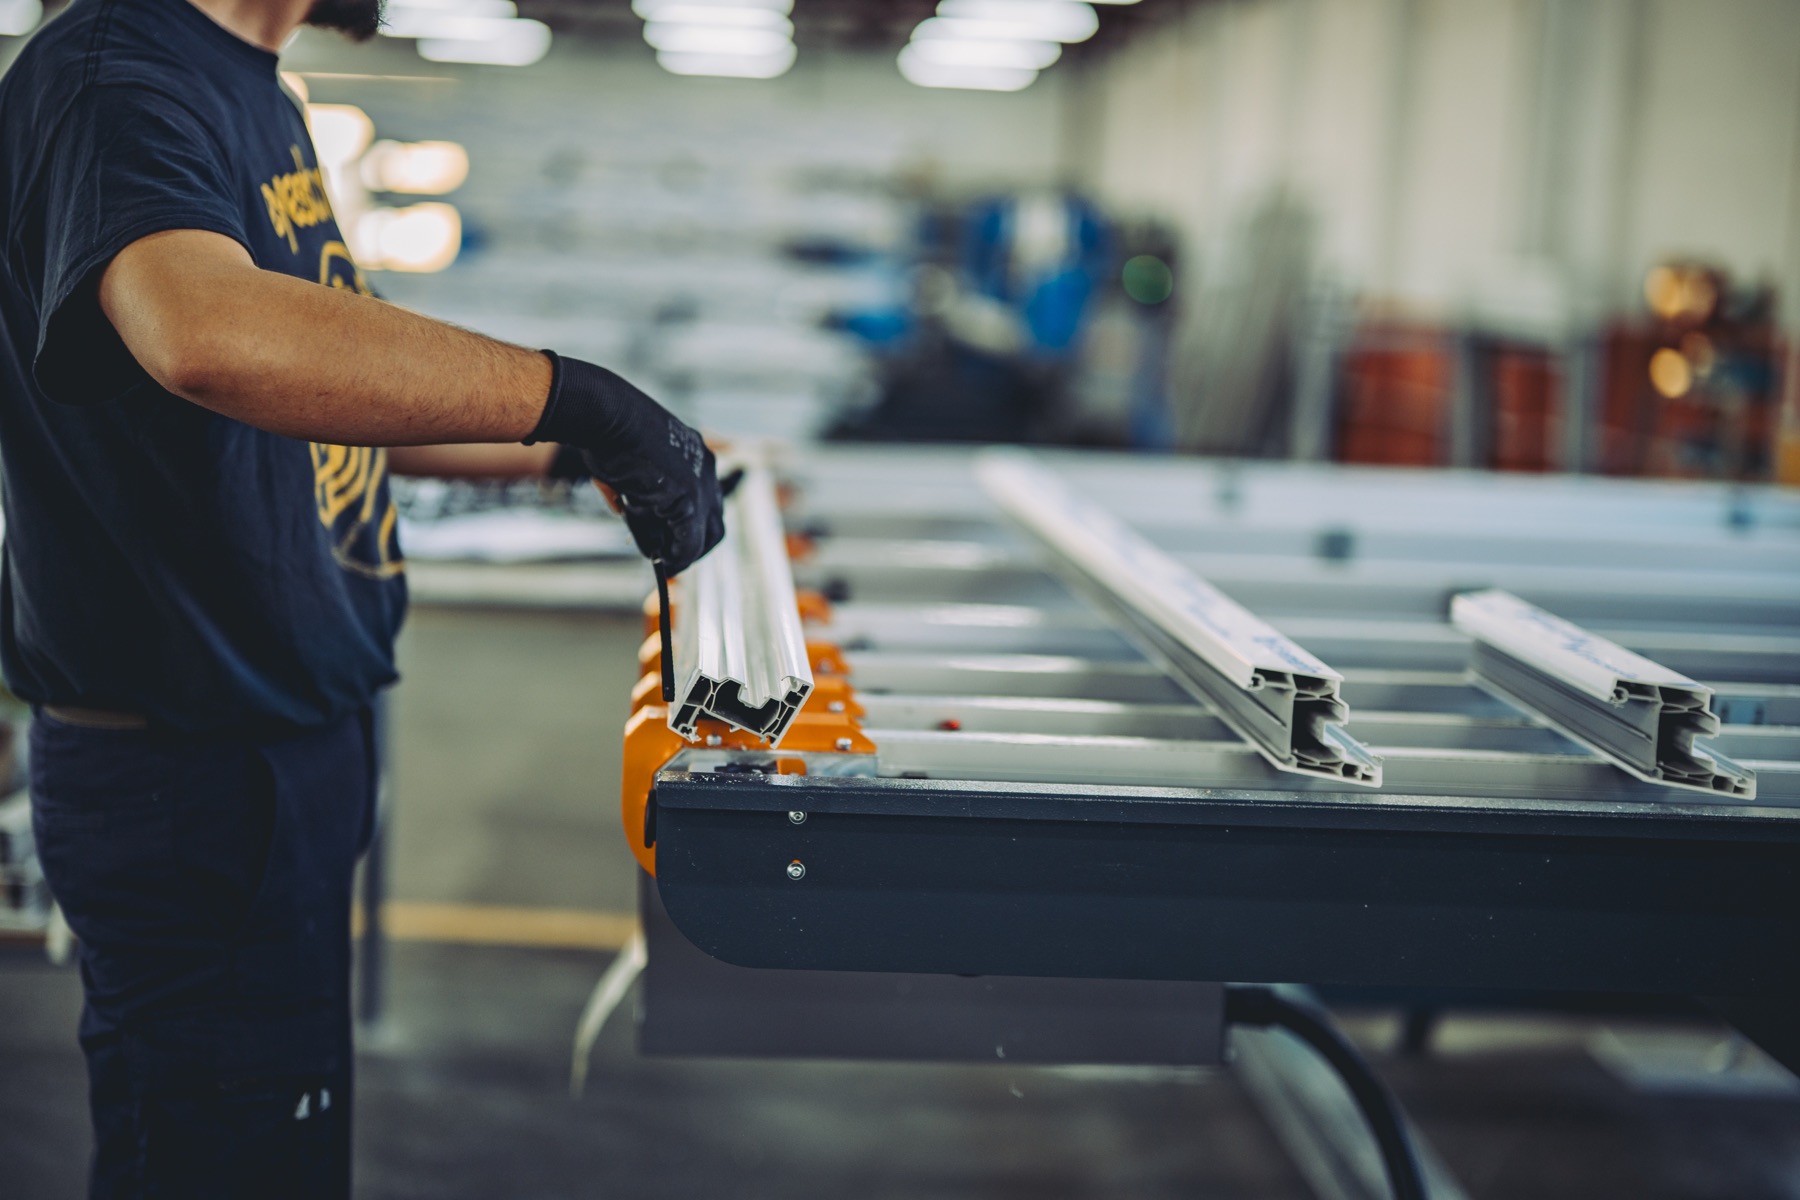
The exact route changes with the alloy pairing, plate area and purchaser specification. These are the controls common to every project.
We align the base and clad grades, thicknesses, dimensions, code requirements and intended fabrication.
Certificates, identity, temper and surface condition are checked before either plate enters production.
Contact faces are prepared and the stand-off geometry is set for the selected collision window.
Controlled energy accelerates the flyer plate into the backing metal, forming a metallurgical interface.
Edge trimming, flattening and any specified heat treatment are sequenced to protect dimensions and properties.
UT mapping, mechanical coupons, dimensions and records are consolidated into the final dossier.
02 / Interface
The collision removes surface films and brings clean metal surfaces together under pressure. The resulting interface geometry depends on material properties and the selected process window.
Process descriptions are general. Acceptance criteria are always taken from the applicable product standard and purchase specification.